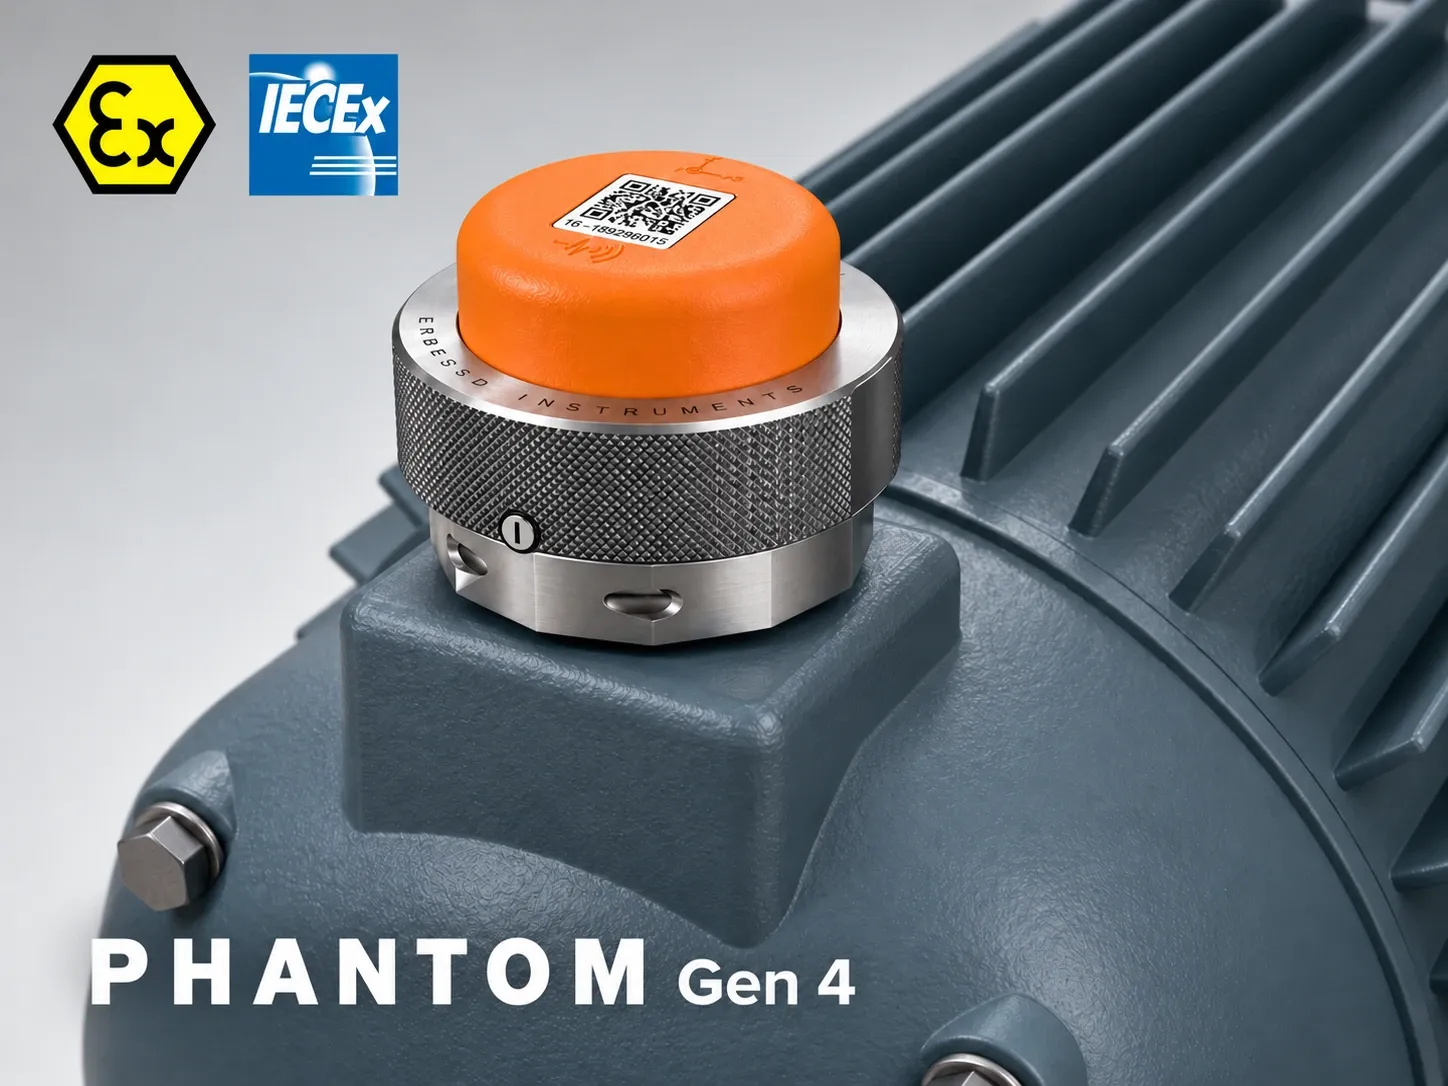
An ATEX certified vibration monitoring sensor for hazardous areas measures machine vibration on rotating equipment installed in classified environments. It is used on motors, pumps, fans, gearboxes, blowers, and similar assets where continuous condition monitoring is needed and where standard electronic devices may not be suitable.
This sensor combines triaxial vibration measurement, wireless data transmission, and hazardous-area certification in one device. The result is a practical way to extend predictive maintenance into gas and dust environments without depending on a wired sensor at every point.
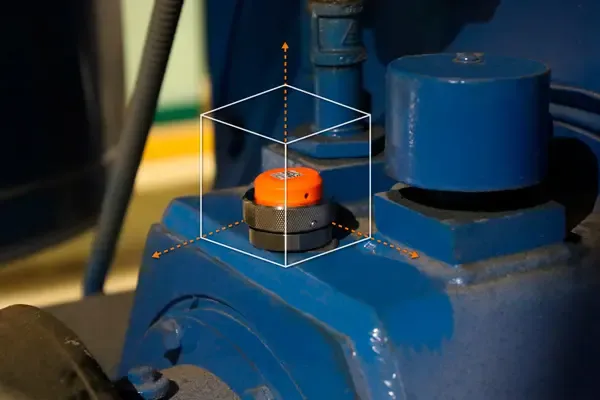
Triaxial vibration measurement for better machine visibility
This gives a broader view of machine behavior than a single-direction reading and improves the ability to track changes in response over time.
Three-axis data is useful when vibration changes with load, structure, mounting condition, or fault type. It also helps when the goal is not only to detect that vibration increased, but to understand how the machine is moving and how that response is evolving.
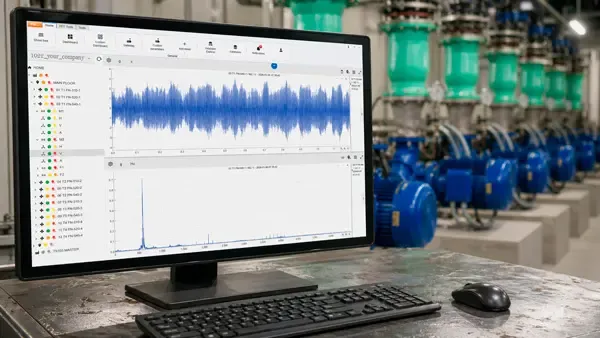
Complete Waveform and FFT data for vibration analysis
Complete waveform and FFT data give the analyst access to the raw vibration behavior of the machine, not only processed overall values. The waveform helps identify impact events, modulation, instability, and repeating patterns, while the FFT helps separate mechanical frequencies, harmonics, sidebands, and high-frequency content associated with specific fault mechanisms.
The analyst can evaluate fault frequencies, harmonic structure, spectral energy distribution, and changes over time to support diagnosis of imbalance, misalignment, looseness, resonance, and bearing-related problems. For condition monitoring, the value is not only that the sensor detects a change, but that it provides enough signal detail for the analyst to interpret the machine response with greater confidence.
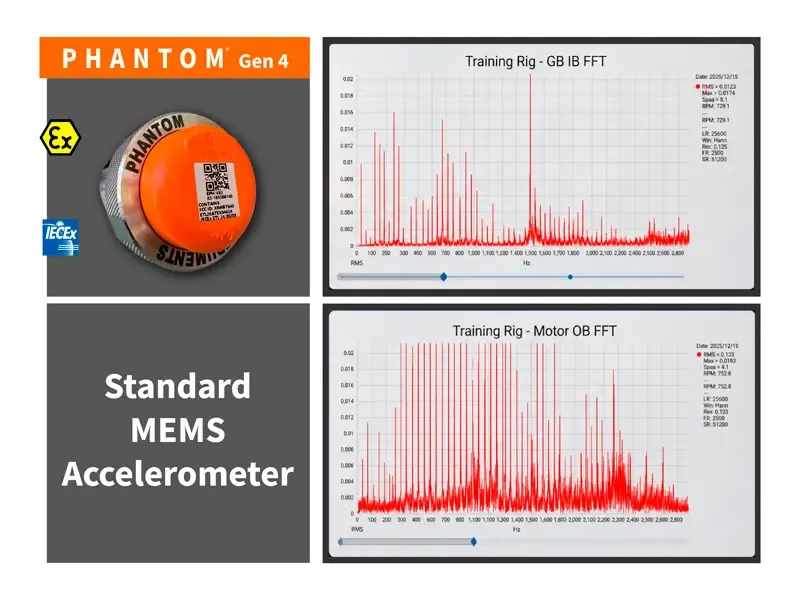
Lower sensor noise for more reliable vibration analysis
Lower sensor noise improves the quality of the vibration signal and makes smaller machine responses easier to distinguish from the sensor background. A lower noise floor allows the analyst to see low-amplitude components with greater clarity, especially in applications where early-stage faults, weaker harmonics, or subtle changes in spectral content would otherwise be masked.
The analyst gains better visibility in the waveform and FFT, which improves the use of diagnostic tools such as harmonic evaluation, sideband review, fault-frequency tracking, spectral comparison, and trend correlation over time.
“With the ATEX certified vibration monitoring sensor for hazardous areas PHANTOM® G4, we’re breaking down one of the last barriers in condition monitoring. It delivers continuous vibration insight in hazardous environments—safely—unlocking critical data from assets that were once considered untouchable and transforming how decisions are made in high-risk operations”
Juan Pablo Mendoza
Erbessd Instruments Director of Development
Technical specifications shared by both versions
| Built-in sensor | Low noise MEMS sensor |
|---|---|
| Sensing resolution (X, Y, Z) | 460 µg |
| Resolution lines | Triaxial 12,800 · Single axis 25,600 |
| Ingress protection | IP69 |
| Certification | ATEX and IECEx (gas and dust) |
| ATEX certificate | ETL 26ATEX0465X |
| ATEX marking | II 3G Ex ic IIC T5 Gc · II 3D Ex ic IIIC T85°C Dc |
| IECEx certificate | IECEx ETL 24.0020X |
| IECEx marking | Ex ic IIC T5 Gc · Ex ic IIIC T85°C Dc |
| Ambient temperature (Ta) | -30 °C to +80 °C |
| Sample rate (configurable) | 32 / 16 / 8 / 4 / 2 / 1 / 0.5 kHz |
| Recording time (3 axes) | 1 s at 32 kHz · 2 s at 16 kHz · 4 s at 8 kHz · 8 s at 4 kHz · 16 s at 2 kHz · 32 s at 1 kHz · 64 s at 0.5 kHz |
| Recording time (1 axis) | 3 s at 32 kHz · 6 s at 16 kHz · 12 s at 8 kHz · 24 s at 4 kHz · 48 s at 2 kHz · 96 s at 1 kHz · 192 s at 0.5 kHz |
High range vs. high sensitivity
| High range · EPH-V83 | High sensitivity · EPH-V82 | |
|---|---|---|
| Frequency range | 0.0 Hz to 8 kHz | 0.0 Hz to 4 kHz |
| Dynamic range (configurable) | ±15 / ±30 / ±60 g | ±4 / ±8 / ±16 g |
| Max frequency (Fmax) by sample rate | 32 kHz → 8 kHz · 16 kHz → 6.25 kHz · 8 kHz → 3.125 kHz · 4 kHz → 1.562 kHz · 2 kHz → 0.781 kHz · 1 kHz → 0.390 kHz · 0.5 kHz → 0.195 kHz | 32 kHz → 4 kHz · 16 kHz → 4 kHz · 8 kHz → 3.125 kHz · 4 kHz → 1.562 kHz · 2 kHz → 0.781 kHz · 1 kHz → 0.390 kHz · 0.5 kHz → 0.195 kHz |
| Spectral noise (X, Y) | 44 µg/√Hz | 20 µg/√Hz |
| Spectral noise (Z) | 55 µg/√Hz | 27 µg/√Hz |
Improved from previous vibration monitoring sensors for hazardous areas
These improvements make the Gen 4 ATEX certified vibration monitoring sensor more useful for vibration analysis in hazardous areas, not only for trend monitoring. Lower spectral noise improves the visibility of low-amplitude vibration components, which helps the analyst distinguish real machine behavior from sensor background. This is especially important when the objective is early fault detection, clearer FFT interpretation, and more confident review of subtle changes over time.
Gen 4 also improves measurement consistency by extending the low-frequency response down to 0 Hz and providing the same maximum frequency on all three axes. In practice, this gives a more uniform triaxial signal, better comparison between directions, and cleaner waveform and spectrum data for diagnostics. The increase in dynamic range also allows the sensor to handle a wider variety of machines and operating conditions without sacrificing signal quality.
PHANTOM® Gen 3 vs. Gen 4
| PHANTOM® Gen 3 | PHANTOM® Gen 4 | |
|---|---|---|
| Maximum frequency (Fmax) | 10 kHz on one axis | 8 kHz on all three axes |
| Maximum amplitude | ±8 / ±16 / ±32 g | ±15 / ±30 / ±60 g |
| Spectral noise | 630 µg/√Hz | 44 µg/√Hz |
| Hazardous-area certification | — | ATEX and IECEx |
Both generations share Bluetooth 5.0, the same dimensions and weight, and the 1/4-28 mounting fastener.